Technical Articles & News

Principles, selection, installation, wiring, accuracy and troubleshooting — plus typical applications in injection molding, hydraulics, wind power and steel.

Latest Technical Articles

How to Set the Injection to Packing Switchover: Time, Pressure or Position

How to Set the Injection to Packing Switchover: Time, Pressure or Position

Same machine, same mould, same material, and the part weight still scatters across shifts. The cause often sits at the instant injection changes to packing, where the amount of material in the cavity is settled. This piece separates time, pressure and position triggering, sets out how the switchover point is decided, what early and late switching each produce, and the quickest way to verify it on the floor.
The Last Few Centimetres: How Cushioning Changes the Reading, and How to Read the Cushion

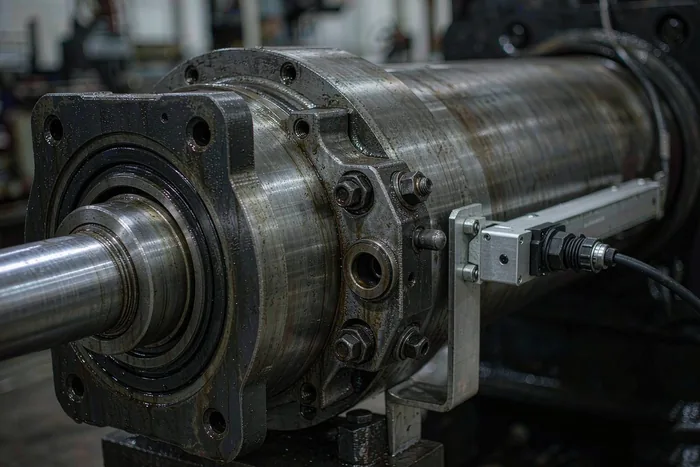
The Last Few Centimetres: How Cushioning Changes the Reading, and How to Read the Cushion

The last few centimetres of a hydraulic cylinder stroke are not travelled at constant speed. Once the cushion collar enters the bore the return flow is throttled and the piston decelerates sharply. That deceleration is written into the position reading: the curve end flattens and the in-position moment moves later. Read the other way, the same segment is a diagnostic window — smooth deceleration is normal, a step or oscillation means the cushion needs attention.

Two Feedback Loops, Not One: Why Spool Position and Cylinder Position Are Measured Separately

Two Feedback Loops, Not One: Why Spool Position and Cylinder Position Are Measured Separately

A servo valve circuit carries two position loops that are easy to confuse. The spool is held by the valve internal feedback and sets response speed. The cylinder needs an externally mounted magnetostrictive displacement sensor and sets where the load finally stops. With only the inner loop, flow offsets from load asymmetry and oil temperature cannot be corrected. This piece separates the two jobs, lists the four checks when selecting the outer unit, and covers the three mistakes most often made on site.

Mould Height and Nozzle Seat: Two Measuring Points That Are Not Like Injection and Clamping

Mould Height and Nozzle Seat: Two Measuring Points That Are Not Like Injection and Clamping

Specifying measuring points on an injection moulding machine often stops at injection, clamping and ejection. Whether the mould height and nozzle seat points are worth adding is usually copied from the next machine along. Mould height is a dimension rather than a travel; the nozzle seat only moves between two ends. This piece separates the five possible points, sets out the three cases that justify a measuring point, and covers the two mistakes most often made when fitting them.

Where to Mount a Magnetostrictive Displacement Sensor: The Wrong Position Moves Both Stroke and Accuracy

Where to Mount a Magnetostrictive Displacement Sensor: The Wrong Position Moves Both Stroke and Accuracy

On the same machine, the reading is always the distance between the fixed end of the rod and the magnet, so where the unit sits is where the datum sits. Mounted on the frame, mounted on the moving carriage, or with both ends moving — the three arrangements measure three different things. This covers what each pattern actually measures, the three checks to run once position is fixed, and how far a measuring line may sit from the axis of motion before angular error starts to dominate.

Replacing a Magnetostrictive Displacement Sensor in a Hydraulic Cylinder: Record Before You Remove

Replacing a Magnetostrictive Displacement Sensor in a Hydraulic Cylinder: Record Before You Remove

Replacing a unit fitted inside a hydraulic cylinder usually goes wrong for two reasons that have nothing to do with technique: nobody recorded the old dimensions before removal, and nobody recalibrated after fitting. This walks through the sequence — the four confirmations before touching anything, the three dimensions and one datum to record while the old unit is still in place, the surfaces that must not be marked during removal, and why recalibration matters more than the swap itself.

A 500 mm Stroke, So Why Order a Longer Range: Working Out Range from Cylinder Stroke

A 500 mm Stroke, So Why Order a Longer Range: Working Out Range from Cylinder Stroke

Ordering range to match the stroke is one of the most common selection errors. A 500 mm stroke ordered as 500 mm leaves both ends unreadable, because nominal range is not usable length — each end carries a fixed dead zone that has to be deducted. This covers the three-step calculation from stroke to ordered range, why the dead zone cannot be estimated from experience, and the checks to run before the order goes out.

Discontinued and Out of Stock: Finding a Replacement Magnetostrictive Displacement Sensor

Discontinued and Out of Stock: Finding a Replacement Magnetostrictive Displacement Sensor

The unit on an ageing machine has failed, the model is out of production, and nobody stocks it. The machine is otherwise fine and the whole job is stuck on one part. This is common in retrofit work and it is solvable, but the order of steps matters. Replacement selection starts with five mechanical dimensions — flange hole spacing, rod diameter and thread, real stroke, pressure rating and wiring form — and only then moves to electrical parameters. Which values must match, which can flex, and what has to be redone after fitting.

Cold and Warm Readings Differ: Thermal Expansion or Magnetostrictive Displacement Sensor Drift

Cold and Warm Readings Differ: Thermal Expansion or Magnetostrictive Displacement Sensor Drift

One reading in the morning, another at noon, a third in the afternoon — and range, zero and wiring all check out. When a cold machine and a warm machine read differently at the same mechanical position, there are two sources: the structure itself is expanding as it heats, and the magnetostrictive displacement sensor drifts with temperature. The two differ by an order of magnitude, and confusing them sends you adjusting in the wrong direction. Three field tests separate them.

How Much Off-Centre Is Too Much: Telling Coaxiality, Parallelism and Squareness Apart

How Much Off-Centre Is Too Much: Telling Coaxiality, Parallelism and Squareness Apart

Walk the full stroke by hand and the reading shudders at one or two fixed stretches while the rest is steady. A new unit behaves the same way. This is rarely the part — it is the rider magnet sitting off-centre on the rod. Eccentricity is not simply a weaker signal: it modulates the return amplitude at the phase where the offset is greatest. Coaxiality, parallelism and squareness are defined first, then how much is allowed, how to measure it, and how to adjust.

Measuring Displacement on a Testing Machine: Pairing with Load and Surviving a Million Cycles

Measuring Displacement on a Testing Machine: Pairing with Load and Surviving a Million Cycles

Displacement measurement on a testing machine is not the same as on a production machine. What is wanted is a zero that is still in place after hundreds of thousands of cycles, and a displacement value that can be matched to a load value at every instant. This covers the three hard requirements, why synchronisation with load matters more than accuracy, and the four places that actually give trouble over long cycling.

Why One Divider Valve Cannot Keep Two Cylinders Together: Four Errors Open Loop Never Corrects

Why One Divider Valve Cannot Keep Two Cylinders Together: Four Errors Open Loop Never Corrects

Two cylinders push the same beam. The command is identical, the valves are identical, and the beam still runs crooked. The problem is not tuning. A divider valve synchronises by splitting flow, and with no position value anywhere in the circuit four errors stay uncorrected: the flow split itself, flow shifting under asymmetric load, oil compressibility, and internal leakage plus oil temperature drift. The position difference keeps accumulating along the stroke until something else stops it.